
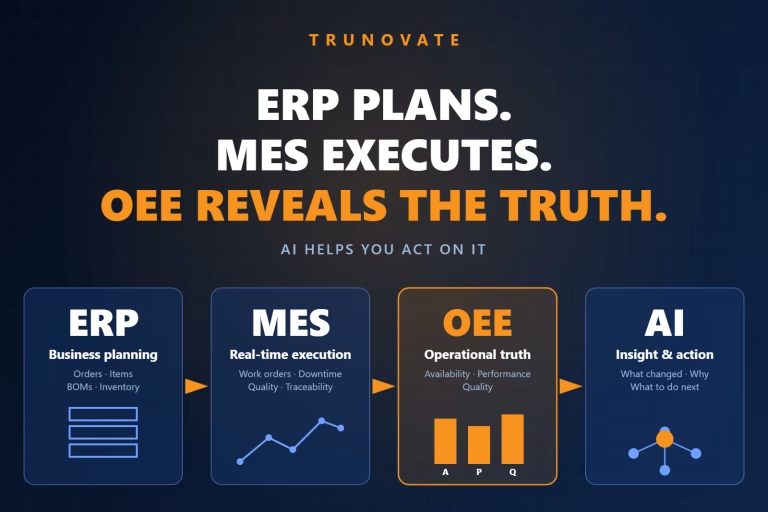
ERP Plans, MES Executes, OEE Reveals the Operational Truth
Lea Tarshish, CEO at Trunovate | PlantSharp MES
In an era where manufacturers are required to respond faster to changes in demand, production disruptions, labor shortages, rising energy costs, and stricter quality requirements, the gap between planning and execution has become one of the key challenges in industry.
Today, almost every manufacturing company manages a significant part of its business activity through an ERP system. The ERP is a central tool for managing orders, purchasing, inventory, planning, costing, finance, and master data. It provides the organization with a broad business view and supports company-level planning.
But when we move down to the production floor, an important gap becomes clear: the ERP knows very well what was planned, but it does not always know what is actually happening right now at the machine, line, shift, or workstation level.
This is where MES comes in.
If ERP is the business planning layer, MES is the operational execution layer. It connects the plan with reality, the work order with actual execution, and the business data with what is happening in real time on the shop floor.
And the metric that helps us understand how effective this execution really is, is OEE.
In the age of AI, this connection becomes even more meaningful: not only collecting data and presenting it in reports, but understanding what changed, why it happened, and what should be done now.
The Gap Between Planning and Execution
In an ERP system, we can see work orders, items, bills of materials, customer orders, inventory, and production plans. These are critical data points for managing the business. But production managers, operations managers, and plant managers often need answers to a different type of question:
- Is the line currently running at the right pace?
- How long was the machine actually available?
- How many stoppages occurred during the shift?
- Does the actual cycle time match the standard cycle time?
- How many products were rejected, and at which stage?
- Is there a bottleneck between workstations?
- Which work order is at risk of delay?
- What is really affecting output?
These are not only planning questions.
They are execution questions.
An MES is designed to address exactly this point. It collects data from the production floor, connects machines, operators, work orders, quality, materials, maintenance, and operational indicators, and helps manufacturers understand what is actually happening, not only what was planned to happen.
Integration Between ERP and MES
The real value is created when ERP and MES do not operate as two separate systems, but as two complementary layers.
The ERP manages the business context: orders, items, customers, inventory, planning, purchasing, and costing. The MES manages the operational context: work order execution, production reporting, downtime, quality, traceability, WIP, maintenance, weighing, and machine data.
Through integration between ERP and MES, work orders, items, BOMs, recipes, and production plans can be transferred to the production floor, while execution reports, output, statuses, consumption, rejects, and quality data are sent back.
This creates a continuous connection between planning and execution.
Instead of managing production based on manual reports, Excel files, or delayed updates, the factory gains a more accurate and up-to-date view of its operational reality. Business planning remains in the ERP, while execution control takes place where production actually happens.
Why OEE Is Such an Important Metric
OEE, or Overall Equipment Effectiveness, is one of the key metrics for understanding production efficiency. It combines three main components:
- Availability: how much time the equipment was actually available for production.
- Performance: whether the line or machine operated at the planned speed.
- Quality: how much of the output was good and produced without rejects.
At first glance, OEE may seem like a simple metric. In practice, it is a powerful management tool because it reveals the main sources of loss in the factory.
A production line may show low output because of multiple stoppages.
A machine may be available, but running below its standard speed.
A product may be produced on time, but with a high reject rate.
A shift may look efficient at a general level, while hiding long changeovers or repeated micro-stoppages.
OEE helps turn assumptions into data. Instead of saying “the line is not performing well enough,” managers can understand whether the issue is related to availability, performance, or quality.
A Practical Example: When an OEE Drop Is Not Just One Number
Let’s assume a production line shows a drop in OEE during the morning shift. At first glance, this appears as one efficiency metric. But behind this number, several very different factors may be hidden.
The line may have suffered from repeated short stoppages, each one appearing insignificant on its own, but together creating a meaningful output loss. Changeover time may have been longer than usual. The line may have been running below the standard cycle time, or rejects may have increased for a specific product.
The managerial meaning of each scenario is completely different.
If the problem is availability, maintenance intervention or equipment availability analysis may be required.
If the problem is performance, the team may need to examine machine speed, work instructions, or operator skills.
If the problem is quality, the team may need to check raw materials, process parameters, a specific batch, or an inspection point.
This is why OEE is not only a metric. It is an entry point for understanding operational loss and making better decisions.
Real-Time OEE, Not Only After the Fact
In many factories, OEE is calculated at the end of a shift, at the end of the day, or in a periodic report. This is better than not measuring at all, but the management value is limited when the information arrives too late.
When OEE is measured in real time, issues can be identified as they happen.
If a production line starts running below the expected speed, this can be identified during the shift. If short stoppages accumulate into a significant loss, this can be seen before the end of the day. If rejects increase for a specific product, the source of the problem can be investigated while production is still running.
The shift from retrospective OEE to real-time OEE changes the way production is managed. It allows managers and operators to act earlier, reduce losses, improve quality, and increase output.
PlantSharp OEE Capabilities
PlantSharp MES enables manufacturers to measure and analyze OEE in real time by connecting production data, machine availability, production speed, output, rejects, and downtime.
The system helps identify the main sources of loss: availability, performance, and quality, and helps determine whether efficiency loss is caused by stoppages, reduced speed, scrap, failures, changeover time, or deviations from plan.
One of the important advantages is the ability to drill down. Instead of looking only at a general OEE score, performance can be analyzed by line, machine, product, work order, shift, or time period. This turns OEE from a reporting metric into a management tool that drives action.
When PlantSharp is connected to ERP systems, machines, PLCs, and additional data sources, it can provide a broader view of performance. Not only how much was produced, but under what conditions, at what pace, with which losses, and where improvement is possible.
From Data to Insight and Action
One of the main challenges in factories is not the lack of data, but the ability to turn data into insights at the right time.
Even when dashboards, reports, and metrics exist, managers still need to understand what changed, what caused it, what it means, and what should be done now.
This is where the AI layer comes in.
PEXA, Trunovate’s operational AI agents layer, is designed to help managers work with manufacturing data in a more natural and focused way. Instead of moving between different reports, managers can ask questions, identify trends, understand exceptions, and receive guidance on topics that require attention.
For example:
- Why did OEE drop during the last shift?
- Which machine generated most of the downtime?
- Is the drop related to availability, performance, or quality?
- Is there a specific product generating more rejects?
- Which work order is at risk of delay?
- Is this a one-time event or a recurring trend?
The value of PEXA is not only in presenting data, but in helping managers understand the operational context and make better decisions.
MES, ERP, and AI: Three Complementary Layers
To manage a modern factory effectively, three main layers need to work together.
ERP provides the business planning layer.
MES provides the operational execution layer.
AI provides a layer of understanding, analysis, and action guidance.
When these three layers are connected, the factory can move from report-based management to real-time, data-driven management. The plan in the ERP receives feedback from actual execution. The MES provides real-time visibility into production. The AI layer helps identify what matters, what is abnormal, and what requires action.
This is not only a technological evolution.
It is a management evolution.
The Path to Continuous Improvement
Production improvement does not always begin with a large and complex project. Sometimes, it starts with one line, one department, or one metric that is measured correctly.
With a modular and focused approach, manufacturers can start with a relatively limited scope, create initial visibility into production metrics, downtime, output, and quality, and then gradually expand to additional lines, modules, and sites. In focused projects, a first production line can go live within approximately 30 days, creating the foundation for an ongoing improvement process.
The important point is not only to implement a system, but to create a new management language around production data.
When managers, engineers, quality teams, maintenance teams, and operations teams look at the same data, understand the same losses, and act based on the same operational picture, the organization can improve performance more consistently.
Conclusion
ERP plans.
MES executes.
OEE reveals the operational truth.
AI helps understand what to do with that truth.
In an era where manufacturers are required to improve output, quality, availability, cost, and response time, the connection between ERP, MES, OEE, and AI is becoming a core foundation for advanced manufacturing management.
PlantSharp MES provides the real-time execution and measurement layer. PEXA adds an operational AI layer that helps turn data into insights and actions.
The factories that will succeed in the coming years will not be the ones that simply collect more data, but the ones that connect it correctly, understand it in time, and act on it faster.
Related reading: Manufacturing Agents: Turning Factory Data into Real-Time Operational Decisions · PlantSharp MES · PEXA Manufacturing Agents · Frequently Asked Questions
Request a Demo
See PlantSharp MES in action.
Our team will walk you through the platform and show you how it can transform your manufacturing operations.
- Personalized Walkthrough - See features tailored to your specific manufacturing needs
- Expert Consultation - Speak directly with our manufacturing solutions specialists
- No Obligation - Free demo with no commitment required